A practical guide from Packaging in Time to help you choose better materials, structure, printing, and finishing for custom boxes.
Cosmetic packaging has to protect a precise primary container and present a controlled retail surface at the same time. A glass serum bottle, pump jar, squeeze tube, compact, and fragrance set place different loads on the box and insert. Custom cosmetic boxes connect those physical requirements with printing, foil, embossing, labeling, shelf presentation, and distribution.
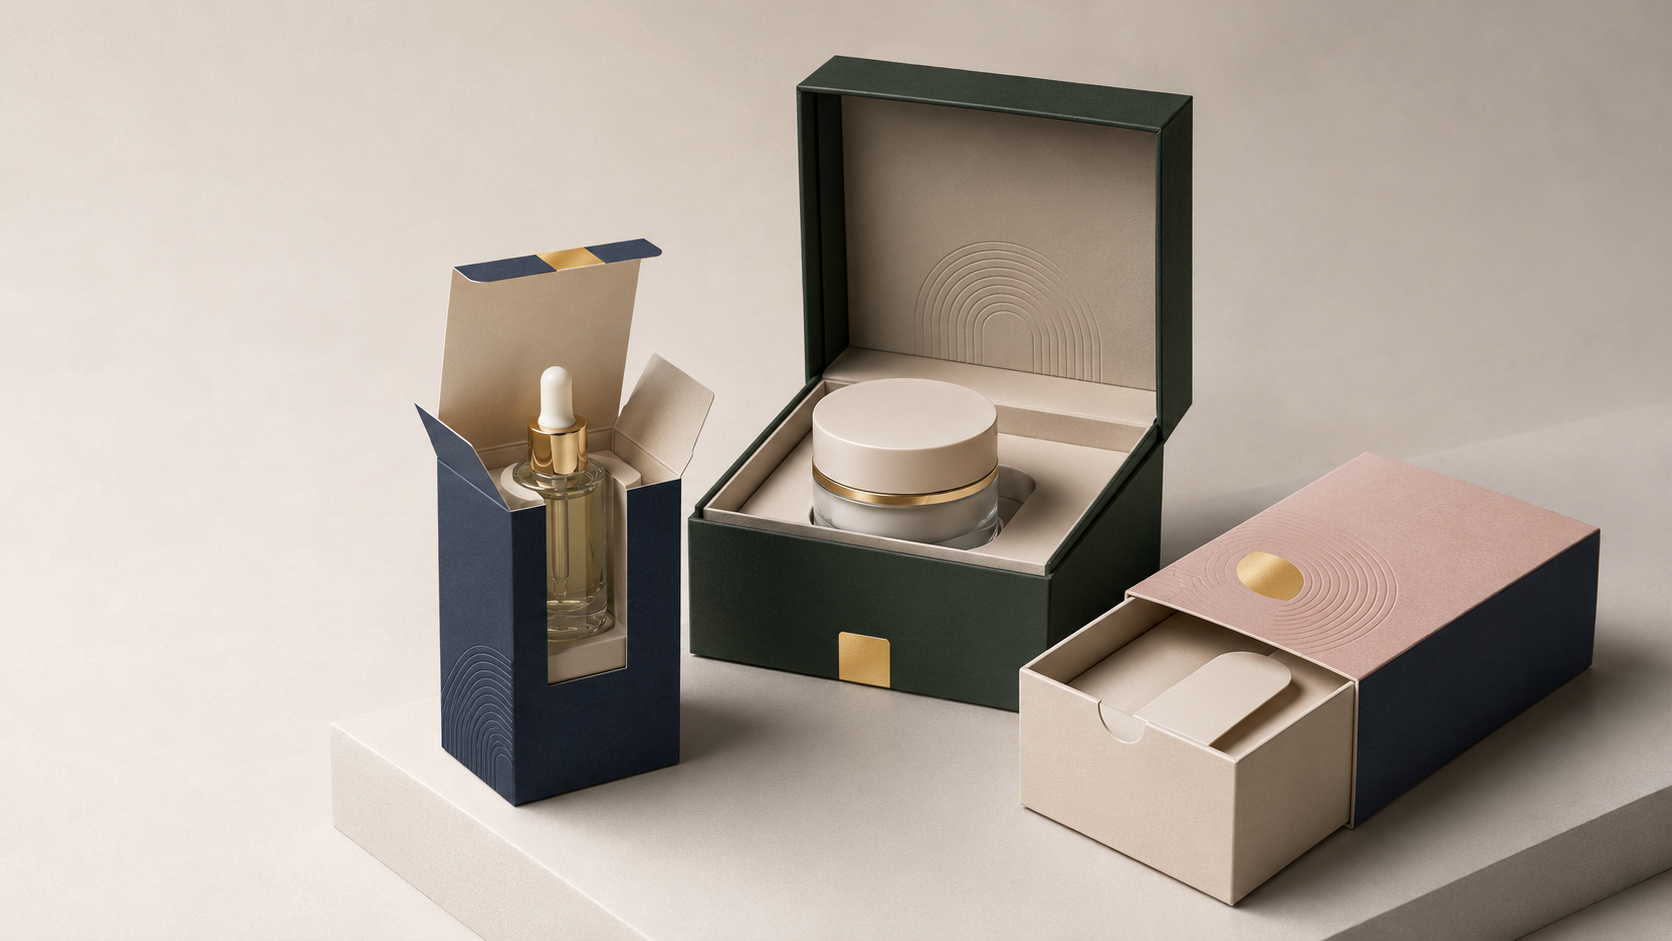
Cosmetic folding cartons provide flat-pack efficiency and detailed print. Rigid cosmetic boxes provide a fixed presentation for sets and higher-value products but require more storage and usually an outer shipping case. Foil stamped cosmetic boxes add a transferred metallic or pigmented film, while embossed cosmetic packaging adds physical relief. Both processes require tooling, registration allowances, and compatible board and coating.
This guide explains structures, dimensions, materials, printing, foil, embossing, coatings, inserts, closures, labeling, sampling, testing, failure modes, and ordering. Buyers can use the sequence to prepare a cosmetic box specification around the actual container, artwork, sales channel, and packing operation.
What Are Custom Cosmetic Boxes?
Custom cosmetic boxes protect and present bottles, jars, tubes, compacts, applicators, and sets while carrying retail graphics and required label information. Most are secondary packages placed around a filled primary container. They can also group several products into a gift or promotional set.
A cosmetic box starts with a dieline or rigid-box drawing. A dieline maps cuts, scores, panels, glue flaps, windows, and artwork on a flat sheet. A rigid-box drawing adds board pieces, wrap paper, joints, turn-ins, lid clearances, and insert geometry. The converter prints and finishes the material, then cuts, folds, glues, wraps, or assembles the box.
The structure must account for the filled product, not only an empty container sample. Fill weight, cap torque, pump height, dropper bulb, product viscosity, label thickness, and production tolerances can change fit. Decoration and labeling are applied after those physical requirements are defined.
Primary Cosmetic Containers Versus Secondary Boxes
The primary container directly holds the cosmetic. Common examples include a glass bottle, plastic jar, squeeze tube, airless pump, compact, lipstick mechanism, vial, or sachet. It controls product containment, dispensing, and much of the product compatibility system.
The secondary box surrounds the primary container. It adds printed area, light blocking, tamper indication, component grouping, impact separation, and retail presentation. It does not automatically prevent a pump from leaking or a glass bottle from breaking.
The shipping case or parcel mailer forms a third level. It protects one or more cosmetic boxes through distribution. A foil stamped folding carton can look suitable for delivery but still need an outer corrugated shipper to prevent crushed corners, abrasion, and moisture exposure.
How Does the Sales Channel Change the Box Specification?
Retail shelves reward a compact footprint, clear product identity, readable copy, and stable forward-facing panels. Department-store counters may require a premium finish, security label, tester relationship, or coordinated set. Subscription programs add recurring fulfillment, version changes, and parcel handling.
E-commerce exposes the packed product to drops, vibration, compression, and repeated orientation changes. A rigid presentation box may still need cushioning and a shipping case. A folding carton can require an insert or neck lock to keep a bottle from striking the walls.
Travel and gift sets group several containers with different shapes and weights. The insert should keep each product located when the box is carried vertically, stored on its side, or opened after distribution. Sales-channel priorities should be ranked before one structure is asked to serve every route.
Which Cosmetic Box Structures Fit Different Beauty Products?
Cosmetic box structures control assembly, presentation, closure, storage, and access for a defined primary container. The best structure follows product geometry, filled weight, label space, decoration, and packing method.
Tuck-End and Auto-Lock Folding Cartons
Tuck-end folding cartons are cut and creased paperboard structures supplied flat. Straight tuck end cartons place top and bottom tuck flaps on the same side. Reverse tuck end cartons place them on opposite sides. Both suit bottles, tubes, jars, compacts, and many single-product retail units.
Auto-lock bottoms use pre-glued base panels that form a lock when the carton opens. They can reduce bottom-assembly steps and provide a stable base for heavier containers. The lock pattern, board caliper, filled weight, and load path should be verified in a sample.
Tuck friction changes with coating, score position, board thickness, and tolerance. A loose tuck can open during handling. A tight tuck can tear print or deform the top panel. Seal labels or tamper-evident features may be added where the product and market require them.
Tray-and-Sleeve Cosmetic Boxes
Tray-and-sleeve boxes use an inner tray that slides into an outer sleeve. The tray can be folding paperboard, rigid board, molded pulp, foam, or thermoformed plastic. The sleeve provides a broad printed or decorated surface.
Friction must hold the sleeve during handling without making it difficult to open. A thumb notch, pull ribbon, or exposed tray edge can support access. Ribbons add another component and can interfere with automated packing or material-recovery goals.
The tray should stop before it exits unintentionally. Product weight and sleeve orientation affect the risk. A vertical shelf display can cause a loose tray to slide, while a tight sleeve can scuff foil or soft-touch surfaces.
Rigid Lid-and-Base and Shoulder Boxes
Rigid setup boxes use dense board, often called greyboard, wrapped with printed or colored paper. Lid-and-base boxes have a separate top and bottom. Shoulder boxes add a raised inner platform or collar that controls lid alignment and creates a visible reveal.
Rigid boxes maintain a fixed shape and support deep fitted inserts. They arrive assembled and occupy more storage and freight volume than folding cartons. Wrapped corners, lid fit, turn-ins, joints, and insert placement create production tolerances that should be sampled.
The box still needs an outer shipper for many distribution routes. Wrapped paper and decorated surfaces can scuff inside a master case. Tissue, sleeves, pads, or protective bags may be used during production and removed before retail presentation, subject to the packing plan.
Hinged and Magnetic Closure Boxes
Hinged rigid boxes connect the lid and base through a wrapped joint. Magnetic closures place magnets and matching metal components within the lid and front wall. The opening path can create a controlled presentation for skincare, fragrance, and gift sets.
Magnet strength, placement, polarity, board thickness, wrap tension, and product weight affect closure. A magnetic lid should not be treated as a transit seal. Tape, a sleeve, a belly band, or an outer case may still be needed.
Magnets and metal pieces change the material construction and disposal instructions. They can also create assembly controls because a reversed magnet or shifted plate produces a closure defect. The inspection plan should include closure alignment and holding behavior.
Window Boxes and Display Cartons
Window cartons use a die-cut aperture to reveal the bottle, jar, tube, or product color. A transparent film can cover the opening, or the aperture can remain open. The window removes board area and creates another adhesive and material interface.
The primary container should remain centered behind the opening. An insert, neck collar, base platform, or side rails can prevent rotation and settling. A clear bottle can show an unintended back panel or insert edge unless the view is planned in three dimensions.
Display cartons and counter trays hold several selling units. Their walls, header cards, and front lips must retain products as inventory decreases. A decorated individual carton and a corrugated display tray perform different structural roles and should be specified separately.
Multi-Product Gift Sets and Promotional Kits
Gift sets place containers of different sizes, masses, and fragility in one insert. A heavy jar can strike a light tube if cavities do not restrain movement. A tall bottle can create leverage on a narrow neck collar.
The opening sequence should make each product removable without collapsing the insert. Finger notches, clearance, pull tabs, and layered platforms control access. Deep cavities can hide labels or create excessive removal force.
Versioning can change one component without changing the outer box. The insert should be checked against the exact set, and the artwork should identify which products, shades, or sizes are included.
Which Structure Works for Both Retail and E-Commerce?
A shared structure can work when the retail box protects the primary container and an outer parcel package handles carrier hazards. The cosmetic box should not be oversized merely to replace a properly designed shipper.
A folding carton with a paperboard insert can provide shelf presentation and product restraint. A corrugated mailer can protect it in parcel delivery. A rigid box can serve as a gift presentation and be placed in a fitted shipping case with cushioning.
The complete packaged product should be tested in each channel configuration. Passing a retail shelf trial does not establish parcel performance, and passing a parcel test does not approve decoration quality after repeated customer handling.
How Should Cosmetic Box Size, Fit, and Orientation Be Specified?
Cosmetic box dimensions and inserts control clearance, movement, pump protection, removal, and shelf footprint. Internal dimensions should be separated from external dimensions and measured in the intended packed orientation.
Internal Dimensions, Product Tolerances, and Headspace
Internal length, width, and depth describe usable space inside the erected box. External dimensions include board thickness, folds, seams, wrap, and construction. A rigid box and a folding carton with the same internal space can have different external dimensions.
Product tolerances should include the smallest and largest primary containers, label overlap, cap variation, fill bulge, and decorative components. A nominal zero-clearance fit can fail when both product and box reach the high side of tolerance.
Headspace protects pumps, droppers, caps, and applicators from top load. Excess headspace permits movement. A top pad, neck collar, shoulder support, or insert wall can locate the container without loading a fragile actuator.
Bottles, Jars, Tubes, Compacts, Pumps, and Droppers
Bottles concentrate weight at their base and can rotate around a narrow neck. Jars have a broad footprint and may need a finger notch beneath the lid. Tubes can flatten, slide, or place pressure on crimped ends.
Compacts can have delicate hinges, mirrors, and decorated surfaces. Pumps and droppers project above the main container and should not carry stacking load. Applicators, spatulas, and brushes require separate cavities or retention tabs.
Filled samples should be used where possible. An empty bottle can have the correct dimensions but the wrong center of gravity. A viscous product can remain at one end of a tube and change how the package lands.
Insert Cavities, Finger Notches, and Removal Force
Insert cavities should restrain the product without scratching labels, coatings, or glass. Paperboard folds can form platforms, side locks, neck collars, and tabs. Molded pulp, foam, and thermoformed trays create other cavity shapes and cushioning levels.
Finger notches provide access at the base, shoulder, or cap. Their position should follow the customer’s grip and avoid exposing fragile components. Removal force should be consistent across product and insert tolerances.
A deep rigid-box cavity can create suction or tight friction around a jar. Relief cuts, tapered walls, pull tabs, or adjusted clearance can improve removal. The solution should be verified after the product and insert have been conditioned and shipped.
How Does Filled Weight Change the Box and Insert?
Filled weight changes base load, drop energy, shelf stability, and carrying force. A paperboard platform that holds an empty jar can bow under the filled product. A magnetic lid that stays closed when empty can open when carried with a heavy set.
Weight distribution also affects orientation. A top-heavy pump bottle can tip inside a shallow tray. A glass bottle placed near the edge of a gift box can twist the insert during a drop.
The specification should state unit weight, set weight, center-of-gravity concerns, and maximum product condition. Testing should use the actual filled weight or a representative mass with equivalent geometry.
Which Materials Work for Cosmetic Packaging Boxes?
Cosmetic packaging materials determine stiffness, print quality, folding, wrap appearance, and insert behavior. Paperboard, corrugated board, and rigid greyboard are different constructions.
SBS Paperboard for Detailed Folding Cartons
Solid bleached sulfate, or SBS, is a white paperboard with a smooth print surface. It supports fine text, process color, spot color, foil, embossing, coating, and precise die cutting.
Caliper affects stiffness, score depth, internal space, fold force, and foil or embossing response. A heavier sheet can support a larger carton but may need different tooling and glue settings.
SBS is often selected for cosmetics because the white surface supports controlled color. The finished result still changes with board shade, coating, ink film, press condition, and lighting.
Kraft and Recycled Paperboard for Defined Surface Goals
Kraft paperboard provides a brown surface and visible fiber character. Printed colors interact with the substrate, and white ink may be used as a base where the press supports the required opacity.
Coated recycled paperboard can support selected secondary cartons. Its reverse-side shade, surface, stiffness, and odor differ by grade. A grey back may be visible through a window or at a tuck end.
Kraft appearance does not prove recycled content, certification, recyclability, or compostability. Each claim needs separate documentation. A premium appearance also depends on the specific print and converting result, not fiber color alone.
E-Flute Corrugated Board for Added Rigidity
E-flute corrugated board combines liners with a thin fluted medium. It provides more wall rigidity than a single paperboard sheet and can suit larger cosmetic sets, counter displays, and e-commerce presentation boxes.
Direct flexographic print, digital print, or litho-lamination can apply graphics. Litho-lamination bonds a separately printed sheet to the corrugated structure. The added layer affects thickness, fold geometry, moisture balance, and converting.
Flute profile alone does not define performance. Liner grades, medium, adhesive, board grade, box style, product weight, and environment all matter.
Greyboard and Wrap Paper for Rigid Boxes
Greyboard forms the core of many rigid setup boxes. Printed, colored, or textured wrap paper covers the core and turns over the edges. The wrap establishes the visible surface while the core provides fixed shape.
Core thickness, joint gaps, wrap stretch, adhesive, turn-in width, corner construction, and drying affect the result. Dark wraps can show adhesive marks, scuffs, or corner variation. Light wraps can show greyboard at exposed edges if coverage is insufficient.
Rigid-box samples should use production-representative core, wrap, finish, and insert where appearance is a primary approval criterion.
Paperboard, Molded Pulp, Foam, and Thermoformed Inserts
Paperboard inserts fold into locks, platforms, and partitions. They can carry print and remain within a fiber-based construction, subject to coatings and adhesives. Their cushioning is limited compared with some foam systems.
Molded pulp forms a fiber cavity and can support irregular shapes. Surface texture and dimensional tolerance differ from die-cut paperboard. Foam provides cushioning and precise cuts but introduces a separate polymer material. Thermoformed trays create repeatable cavities and can use transparent or colored plastic.
Insert choice should balance fragility, presentation, removal, surface protection, material goals, and packing labor. No insert material is universally preferable.
Which Material Changes Require a New Sample?
Material changes require review when they affect fit, fold, color, foil transfer, embossing, glue, wrap, odor, scuffing, or product protection. A board with the same nominal caliper can have a different surface, stiffness, or score response.
A new wrap paper can stretch or show adhesive differently. A new foam density can change cavity grip. A new window film can change clarity and static. A coating change can alter foil adhesion and rub.
Change records should identify the old and new supplier, grade, specification, approved attributes, and required tests. Generic substitution without evidence can invalidate an approved sample.
How Are Custom Cosmetic Boxes Printed?
Printing applies brand graphics, product information, and machine-readable content to defined carton panels. Process selection depends on substrate, quantity, artwork versions, color target, detail, and finishing.
Digital and Offset Printing for Folding Cartons
Digital printing transfers artwork without conventional plates. It supports short setups and multiple versions, subject to press, substrate, ink, coating, sheet size, and finishing limits.
Offset lithography uses plates and a blanket to print detailed graphics on paperboard or wrap sheets. It can support repeat color control and long runs. Neither method guarantees a specific color or price without a defined job.
The quote should state box size, material, quantity, versions, print coverage, interior print, color references, coating, foil, embossing, and delivery schedule.
CMYK, Spot Colors, White Ink, and Physical Color References
CMYK process printing combines cyan, magenta, yellow, and black to reproduce images and many colors. Spot colors use specified inks or references for selected brand targets. A CMYK conversion simulates a spot color rather than using the same ink.
White ink can form a base on kraft, colored paper, metallic board, or clear film. Opacity and registration vary with the ink system, substrate, and number of passes.
Color approval should state the physical reference, substrate, coating, viewing light, and tolerance method. A monitor image cannot verify a printed metallic, matte, or textured surface.
Interior Printing, Reversed Panels, and Artwork Orientation
Interior printing can add instructions, set information, or color inside a folding carton. It also changes ink coverage and production setup. Glue and insert contact areas may require exclusions.
Reversed panels can appear upside down after folding if orientation is not checked on an assembled sample. The bottom flap, side seam, window, and opening direction should be reviewed in three dimensions.
Artwork layers should separate dieline, varnish, white ink, foil, embossing, cutouts, codes, and nonprinting notes. Production files should not flatten technical layers into the visible design.
How Do Substrate and Coating Change Brand Color?
Substrate shade changes the light reflected through ink. White SBS, brown kraft, colored wrap, recycled board, and metallic stock produce different results from the same color values.
Coatings change gloss and apparent saturation. Matte surfaces scatter light, while gloss surfaces create reflections. Soft-touch treatments can deepen some colors and reveal fingerprints or rub.
Physical proofs and production samples should represent the intended substrate and finish. A proof on white coated paper does not approve the same artwork on kraft or textured wrap.
How Do Foil Stamping and Embossing Work on Cosmetic Boxes?
Foil transfers a decorative film, while embossing changes the physical relief of the printed surface. These are converting processes with tooling, registration, and material constraints.
Hot Foil, Cold Foil, Digital Foil, and Metallic Ink
Hot foil stamping uses a heated die and pressure to release foil from a carrier onto the substrate. It can create metallic, pigmented, holographic, or other effects. Temperature, pressure, dwell, die, foil, coating, and paper surface control transfer.
Cold foil uses an adhesive applied in the desired image and transfers foil from a web, often within a printing process. Digital foil or embellishment applies effects without a conventional stamping die, subject to the equipment and design.
Metallic ink contains reflective pigments and prints like an ink. It does not create the same continuous film or mirror response as foil. The choice should be based on a physical sample and production method.
Embossing, Debossing, Blind Embossing, and Registered Embossing
Embossing presses paperboard between matched tooling to raise a selected area. Debossing presses an area below the surrounding surface. Blind embossing creates relief without printed ink or foil in the raised area.
Registered embossing aligns the relief with printed or foil artwork. Registration tolerance becomes more visible around fine outlines and small text. Board caliper, fiber direction, coating, and image geometry affect relief.
Deep relief can distort the reverse side or thin a coating. Folding cartons need enough clearance from scores, cuts, glue flaps, windows, and panel edges.
Tooling, Registration, Minimum Detail, and Relief Depth
Foil and embossing dies are production tools. Their cost, lead time, repeat use, storage, and ownership should be stated in the quote. Digital embellishment can reduce conventional tooling but has its own limits.
Minimum detail depends on the foil, substrate, die, press, coating, and design. Fine reversed lines can fill, tiny serif type can bridge, and textured paper can prevent complete transfer.
Relief depth should be approved on the intended material. A screen rendering cannot show the tactile result or reverse-side distortion. The supplier should recommend practical allowances for the selected equipment.
Where Should Foil and Embossing Be Kept Away From Folds and Glue?
Foil near a score can crack or lift as the panel folds. Embossing across a score can change fold geometry and weaken the visual alignment. Both effects can interfere with glue if they enter the bonding area.
Window edges, perforations, small tabs, and tuck slits also need clearance. A die impression too close to a cut can distort the edge or reduce strength.
Technical artwork should show foil and embossing as separate spot-color layers. The dieline review should confirm clearances before tooling is ordered.
What Can Cause Foil Cracking, Flaking, or Poor Transfer?
Poor foil transfer can result from incompatible coating, rough paper, insufficient or excess temperature, pressure, dwell, or an unsuitable foil grade. Dust and surface contamination can create missing areas.
Cracking and flaking can occur when foil crosses a score, the substrate bends sharply, or adhesion is incomplete. Large solids and fine detail can need different settings.
Production approval should inspect edges, fill, pinholes, registration, rub, folding, and repeated handling. A flat stamped sheet should be folded into the actual carton before approval.
Which Coatings and Finishes Suit Beauty Packaging?
Coatings and laminations change gloss, touch, abrasion response, glue compatibility, and disposal conditions. They should be selected for a defined surface function.
Matte and Gloss Lamination
Lamination bonds a film to the printed sheet. Matte film reduces surface reflection and can create a smooth feel. Gloss film increases reflection and can deepen color. Both add another layer and can affect folds, glue, foil, codes, and recycling.
Film selection should account for scuffing, fingerprints, curl, and foil compatibility. A matte film can show burnishing where surfaces rub. A glossy film can create barcode glare.
Aqueous Coating, Varnish, Spot UV, and Soft-Touch Surfaces
Aqueous coating is a water-based coating applied and dried on press or in a finishing step. Varnish is a printed coating that can control gloss or protection. Spot UV cures a localized coating with ultraviolet energy to create contrast.
Soft-touch surfaces use a coating or film to create a low-friction tactile effect. The exact construction affects durability, glue, foil, fingerprints, and material recovery.
Localized finishes require registration with printed artwork. Fine spot UV around small type or foil can reveal even minor misalignment.
Anti-Scuff Needs for Dark Colors and High-Contact Panels
Dark solid colors show light scratches, edge rub, and fingerprints more readily than many lighter designs. High-contact panels include lids, sleeve edges, tuck flaps, corners, and surfaces touching master cases.
An anti-scuff target should be tested on the production construction. Coating names do not establish a universal result. Case fit, tissue, protective bags, packing method, and warehouse handling also affect damage.
Rub testing should include decorated areas and finished folds. A surface can pass flat-sheet rub and still mark at corners after packing.
How Do Finishes Affect Glue, Coding, Barcodes, and Recycling?
Glue needs a compatible bonding surface. Lamination, heavy coating, foil, silicone contamination, and soft-touch layers can reduce adhesion. Dielines should reserve glue exclusions where required.
Batch and lot codes need a surface compatible with the coding method. Glossy or low-energy films can reduce ink adhesion. Barcodes need contrast, quiet zones, and limited glare.
Foils, films, magnets, plastic windows, foam, and mixed-material inserts can change recycling instructions. Environmental claims should reflect the complete construction and local acceptance rather than the appearance of the paper surface.
How Do Inserts and Closures Protect Cosmetic Products?
Inserts restrain the primary container, while closures control access and keep the package assembled. They should be designed and tested as one system.
Product Retention for Glass, Pumps, Caps, and Applicators
Glass containers need separation from hard edges and other products. Neck collars can hold bottles upright, while base platforms distribute weight. Side rails can prevent rotation.
Pumps and droppers need headspace and should not carry closure load. Caps should remain accessible for removal but protected from impact. Applicators need separate retention so they do not scratch the container.
The insert should avoid label abrasion and pressure on decorative surfaces. Filled-product drop and vibration trials reveal movement that a static fit check cannot show.
Paperboard Platforms, Neck Collars, and Layered Inserts
Paperboard platforms use folds and locks to create raised cavities. Neck collars hold a narrow portion of a bottle. Layered inserts stack paperboard or rigid components to create depth.
Load paths should transfer weight to the base rather than to a pump or fragile shoulder. Glue tabs and locks should remain outside visible cavities where possible.
Packing teams should be able to identify the correct orientation and load products without forcing them. Line-side samples and visual instructions can reduce reversed inserts and damaged containers.
Magnetic Lids, Tuck Flaps, Sleeves, and Tamper-Evident Seals
Magnetic lids provide repeatable opening and closing but do not necessarily provide tamper evidence. Tuck flaps close folding cartons through friction or locking cuts. Sleeves add retention around trays or rigid boxes.
Tamper-evident labels, seals, perforated tabs, or glued closures show visible disruption. Their design should reflect product requirements, retailer expectations, and the brand’s approved claim.
Closures should be tested after decoration and conditioning. Coating and foil can change tuck friction, while wrap and magnet position can change rigid-box closure.
Where Can Leakage, Product Migration, or Closure Failure Begin?
Leakage can begin at a loose cap, pump, dropper, tube crimp, jar thread, or primary-container defect. The box may then absorb oil, fragrance, alcohol, cream, or serum. Stains can spread through cut edges and glue seams.
Product migration occurs when the insert allows movement. Vibration can rotate a bottle, release an applicator, or push a cap against the lid. A heavy set can distort a platform.
Closure failure can result from poor glue, loose tucks, shifted magnets, sleeve clearance, or product load. Diagnosis should preserve the failed package and record orientation, temperature, route, and lot.
What Labeling Information Belongs on a Cosmetic Box?
Cosmetic box labeling assigns required statements to the principal display and information panels under current rules. The responsible person and regulatory team approve content, while the supplier reproduces the approved artwork.
Principal Display Panel, Identity Statement, and Net Quantity
The principal display panel, or PDP, is the panel most likely to be displayed or examined under customary retail conditions. FDA cosmetic rules require an identity statement and accurate net quantity statement on the PDP.
The identity statement indicates the nature or use of the cosmetic through a common or usual name, descriptive name, understood name, or illustration. The net quantity statement follows placement and format rules. When the cosmetic is sold in an outer container, the outer box is part of that labeling system.
Windows, foil, embossing, and large logos reduce available label space. The regulatory zones should be reserved on the dieline before decoration is finalized.
Business Details, Ingredient Declaration, Warnings, and Directions
Cosmetic labels identify the name and place of business of the manufacturer, packer, or distributor under the applicable requirements. Ingredient declarations generally appear on the outer container when the product is sold in one.
Ingredients follow naming and order rules, including provisions for color additives and ingredients at one percent or less. Product-specific warnings and directions may be required to prevent misuse or health hazards.
Small packages can have specialized allowances, but limited space should not be assumed to remove requirements. The responsible business should review the exact product and package.
MoCRA Responsible-Person and Adverse-Event Label Control
MoCRA defines the responsible person as the manufacturer, packer, or distributor whose name appears on the label. The law added facility registration, product listing, safety substantiation, adverse-event reporting, and other responsibilities, subject to applicable provisions and exemptions.
FDA states that a serious adverse-event report includes a copy of the label on or within the retail packaging. Label version control therefore supports traceability. The responsible person must also provide a channel through which adverse events can be received under the applicable requirements.
Current FDA guidance and legal advice should control the final copy. A packaging supplier can reserve the approved area and track revisions but should not select the responsible person or write regulatory statements without authorization.
Cosmetics That Are Also Drugs
Some products meet both cosmetic and drug definitions based on intended use and claims. Sunscreens, acne treatments, antiperspirants, anti-dandruff products, and certain toothpastes are common examples.
These products must meet applicable drug labeling and other requirements in addition to cosmetic rules. A beauty-style carton layout should not be reused without confirming product classification and the required Drug Facts or other content.
Claims can change classification. The responsible regulatory team should approve product name, benefits, directions, warnings, and promotional copy before print.
Barcodes, Batch Codes, Lot Codes, and Retailer Marks
Retail barcodes need sufficient contrast, quiet zones, size, and placement away from folds, seams, windows, foil, and reflective coating. GS1 and retailer specifications should define the final symbol.
Batch and lot codes connect finished products to production records. The code area should suit the coding equipment and remain accessible after packing. Dark coatings and films can require a dedicated light patch.
Retailer marks, security labels, price labels, and country-specific stickers should not cover required copy. Their planned locations belong on the artwork and packing specification.
Who Approves the Final Cosmetic Label?
The responsible cosmetic business and its qualified regulatory advisers approve the final label. The packaging supplier controls reproduction of the approved version and should maintain file, proof, and production traceability.
The FDA Cosmetics Labeling Guide and 21 CFR Part 701 provide federal requirements, but state, product, drug, retailer, and market rules can add obligations.
A digital proof confirms visible content and placement. It does not prove legal sufficiency, final color, foil transfer, emboss depth, structure, or distribution performance unless those decisions are approved separately.
How Should Cosmetic Packaging Be Sampled and Tested?
Cosmetic packaging should be sampled and tested with the filled primary container, production materials, decoration, and intended distribution route. Each approval method answers a separate question.
Digital Proofs, Structural Samples, and Production Samples
A digital proof checks text, imagery, panel orientation, barcode data, foil and emboss layers, and general color intent. A structural sample checks fit, insert, closure, loading, and opening.
A production sample represents more of the intended board, wrap, ink, coating, foil, embossing, glue, window, and insert. The approval record should state which elements are production-representative.
Complex gift sets may need staged samples: blank structure, decorated carton, fitted insert, packed product, and distribution sample. Approving all variables at once makes failure diagnosis harder.
Foil, Embossing, Color, and Finish Approval
Foil approval should inspect shade, reflectivity, fill, edges, pinholes, registration, adhesion, and fold behavior. Embossing approval should inspect alignment, depth, sharpness, reverse-side distortion, and effect on assembly.
Color approval should identify the substrate, coating, reference, and viewing condition. Finish approval should include rub, fingerprints, gloss, texture, and glue compatibility.
Physical samples provide stronger evidence than renderings for metallic and tactile effects. Approved samples should be stored and labeled with the production version they represent.
Packed-Product Drop, Vibration, Compression, and Leakage Trials
Packed-product testing evaluates the cosmetic, primary container, insert, box, and shipper as one system. Drops can reveal glass contact and insert release. Vibration can loosen pumps, caps, applicators, and sleeves. Compression can bow lids or load actuators.
Leakage trials should use filled products or justified substitutes and include expected orientations and temperatures. The outer box should be inspected for staining, glue loss, window clouding, and finish damage.
The selected distribution test should match the sales route. A retail master case and an individual parcel shipper can require different test plans.
Retail Rub, Scuff, Barcode, and Shelf Tests
Retail tests should include repeated handling, shelf contact, tester placement, security labels, and barcode scanning. Dark matte cartons and foil areas should be observed under store lighting.
Rub and scuff tests should represent contact with master cases, adjacent cartons, shelves, and hands. A pristine sample does not show how the package looks after replenishment.
Shelf trials should check facings, stability, product identity, label visibility, window view, and removal. Gift sets should remain stable at full and partial inventory conditions where applicable.
What Does a Passing Test Not Prove?
A passing drop test does not approve cosmetic labeling. A barcode verification does not approve color or foil. A structural sample does not prove production finish. A rub test does not establish parcel protection.
Tests apply to the product, package, method, conditions, and acceptance criteria used. Changes to the primary container, fill, insert, board, wrap, coating, foil, closure, case pack, or route can require review.
Approval records should keep content, color, structure, finish, distribution, and regulatory decisions separate while connecting them to the same version.
What Common Problems Affect Custom Cosmetic Boxes?
Custom cosmetic box problems usually trace to product fit, material, decoration, artwork, packing, or route. The failed package should be preserved with its product and lot information.
Scuffed Print, Fingerprints, Rub, and Color Variation
Scuffing occurs where cartons contact equipment, cases, shelves, or other cartons. Fingerprints are more visible on some dark, gloss, metallic, and soft-touch surfaces. Rub can polish matte areas or mark foil.
Color varies with board, wrap, ink, coating, press, batch, and viewing light. A screen value does not establish a physical target.
Corrective action can involve coating, ink, case fit, protective interleaving, packing method, cure, or handling. Adding finish without identifying the abrasion source can create another compatibility issue.
Loose Inserts, Broken Glass, Scratched Containers, and Leaks
Loose inserts permit product movement and impact. Tight inserts can scratch labels, coating, or glass and can load pumps. Breakage risk rises when heavy containers can strike rigid walls or each other.
Leaks can stain paperboard and damage glue, windows, foil, and soft-touch coatings. The box cannot correct an unsuitable primary closure, but it can restrain orientation and contain selected secondary effects.
Failure analysis should record filled weight, orientation, temperature, insert position, cap or pump condition, and shipping route.
Foil Misregistration, Emboss Distortion, and Cracked Scores
Foil misregistration can result from sheet movement, die setup, material stretch, or tolerance accumulation. Emboss distortion can occur around fine details, panel edges, and deep relief.
Cracked scores can expose fiber and break ink, coating, or foil. Board grain, caliper, score geometry, moisture, and coating flexibility affect the fold.
The approved sample should be an assembled carton, not only a flat sheet. Production inspection should include folded decorated areas.
Missing Label Copy and Mixed Artwork Versions
Missing copy often results from late layout changes or uncontrolled versions. A larger logo, window, foil block, or retailer label can displace ingredients, warnings, net quantity, or code areas.
Mixed versions can place the wrong shade, size, ingredients, barcode, or language on a box. A master list should connect SKU, product name, formula, container, box size, file revision, and quantity.
Obsolete cartons should be controlled after formulation or label changes. Physical usability does not make an old label current.
Excess Material and Unsupported Environmental Claims
Excess material can result from oversized boxes, deep unused cavities, redundant sleeves, heavy board without a defined load, or a retail box designed to replace a shipper.
Environmental claims about recycled content, recyclability, compostability, plastic-free construction, or certified fiber require specific evidence. The FTC states that claims about products or packaging should be truthful and supported.
Foil, lamination, magnets, windows, foam, adhesives, and mixed inserts should be included in the assessment. A paper appearance does not establish universal recyclability.
How Do You Order Custom Cosmetic Boxes?
Ordering custom cosmetic boxes starts with the filled primary container and sales route. The supplier then translates those requirements into structure, material, insert, print, finishing, samples, tests, production, and delivery.
Document the Product, Primary Container, Channel, and Label Requirements
Product data should include primary-container dimensions, filled weight, material, cap, pump, dropper, applicator, fragile areas, leakage risk, label thickness, and surface sensitivity. Supply the smallest and largest expected conditions.
Channel data should identify shelf, counter, gift set, subscription, e-commerce, travel, or promotional use. Distribution data should identify master case, parcel shipper, pallet, destination, and test requirements.
Label data should identify the principal display panel, information panel, identity, net quantity, business details, ingredients, warnings, directions, adverse-event contact, barcode, batch code, and retailer marks approved for the product.
Confirm Structure, Material, Insert, Print, and Finishing
The structural specification should state the box style, internal dimensions, board, caliper, wrap, lid fit, window, closure, insert material, cavity geometry, and tolerance.
The print specification should state digital or offset route if prescribed, exterior and interior coverage, CMYK, spot colors, white ink, and physical color reference.
The finishing specification should state lamination, coating, foil type and area, embossing or debossing, registration, spot UV, texture, glue exclusions, code areas, and barcode surface.
Approve Samples, Tests, Production Controls, and Delivery
The sample plan should identify digital, structural, color, foil, embossing, finish, production, and packed-product approvals. The test plan should cover fit, removal, closure, leak exposure, rub, scuff, glue, barcode, distribution, and shelf handling.
Production controls should identify final files, tooling, material codes, inspection criteria, version quantities, case pack, protective packing, and obsolete-material rules.
Delivery planning should account for flat versus assembled volume, rigid-box storage, case dimensions, pallet height, split shipments, warehouse conditions, and launch dates.
What Should a Complete Quote Request Include?
A complete request should include:
Filled primary-container dimensions, weight, material, closure, and samples
Product fragility, leakage risk, surface sensitivity, and orientation
Sales channel, retail position, distribution route, and shipper relationship
Box structure, internal dimensions, closure, and required headspace
Board, caliper, flute, greyboard, wrap paper, window, and insert material
Exterior and interior print coverage, CMYK, spot colors, and white ink
Foil type, foil area, embossing or debossing, depth, and registration needs
Lamination, coating, spot UV, anti-scuff, glue, coding, and barcode needs
Required label panels and approved artwork versions
Quantity by size, SKU, shade, set, language, and design
Digital proof, structural sample, color proof, production sample, and tests
Case pack, protective packing, pallet, delivery destination, and schedule
Price, minimum quantity, and lead time depend on the combined scope. Structure, material yield, tooling, print setup, foil, embossing, hand assembly, insert production, version count, testing, packing, and freight can all change the job.
Specify Custom Cosmetic Boxes Around the Primary Container and Sales Channel
Custom cosmetic boxes should be specified around the filled primary container and its complete sales route. Structure comes first, followed by internal dimensions, insert geometry, board, printing, foil, embossing, coating, closure, and label space. Cosmetic folding cartons, rigid cosmetic boxes, foil stamped cosmetic boxes, and embossed cosmetic packaging solve different presentation and handling problems, so the correct format depends on product weight, fragility, leakage risk, retail position, fulfillment, and distribution.
The final file should identify the bottle, jar, tube, compact, pump, applicator, or set; the minimum and maximum dimensions; filled weight; box style; material; insert; print process; color reference; decoration; barcode and code areas; required label panels; artwork versions; sample plan; test route; case pack; pallet; and delivery requirements. Structural samples verify fit and removal. Production-representative samples provide stronger evidence for color, foil, relief, coating, and wrap quality.
Packaging in Time can review a complete specification and prepare a structure, dieline, sample, and quote path. Submit the primary-container dimensions, filled weight, quantity, artwork, finishing, labeling, channel, packing, and delivery requirements to compare suitable cosmetic box options.